
Handle full or empty bottles, cans, jars and similar containers up to 2,000 units per minute!
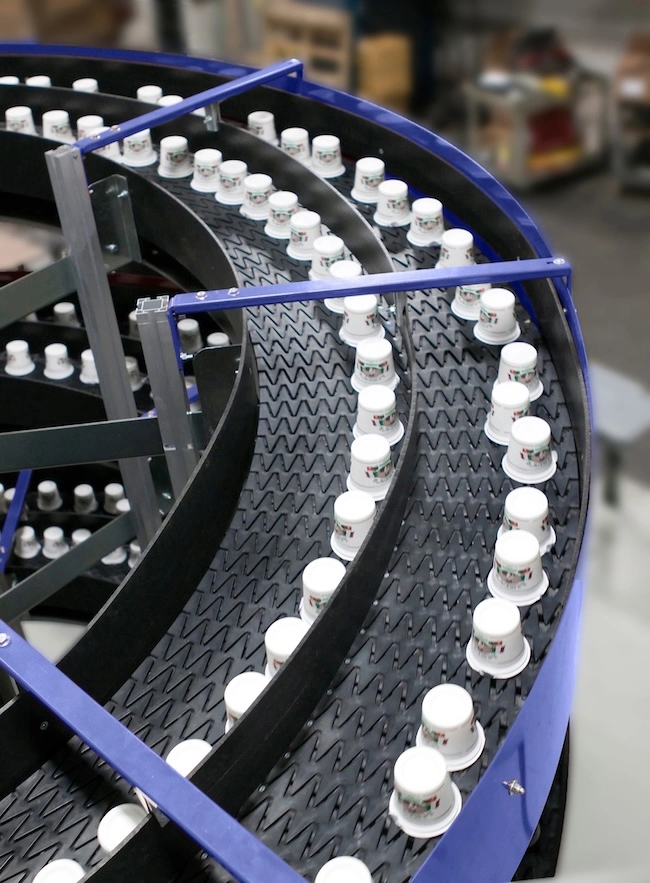
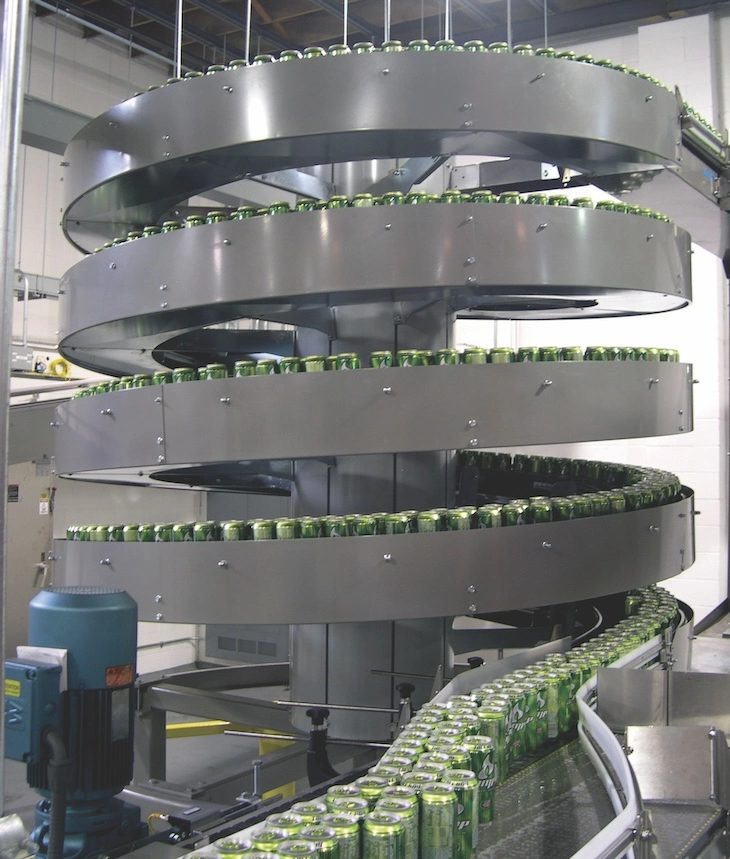
The Apollo Mass Flow Spiral Conveyors are an ideal solution for handling full or empty bottles, cans, jars, other similar single containers. The products are conveyed vertically in a continuous mass flow and similar to our other Spiral Conveyors, it saves valuable floor space by means of vertical transportation.
How it works
The design of our Mass Flow Spiral Conveyor is based on the already proven and reliable Apollo Spiral technology: Like our conventional Spiral Conveyor, the Mass Flow Spiral Conveyor runs with only one motor. Products are conveyed towards the spiral and guided into it with a smooth side transfer. Products are then transported with a smooth and gentile incline. At the desired elevation level the product is then gently guided off the spiral in another smooth side transfer. All Apollo Spiral Conveyors can convey up or down and can optionally be reversible. The Mass Flow Spiral Conveyor can be integrated with your other line components for the most efficient material handling solution.
Characteristics
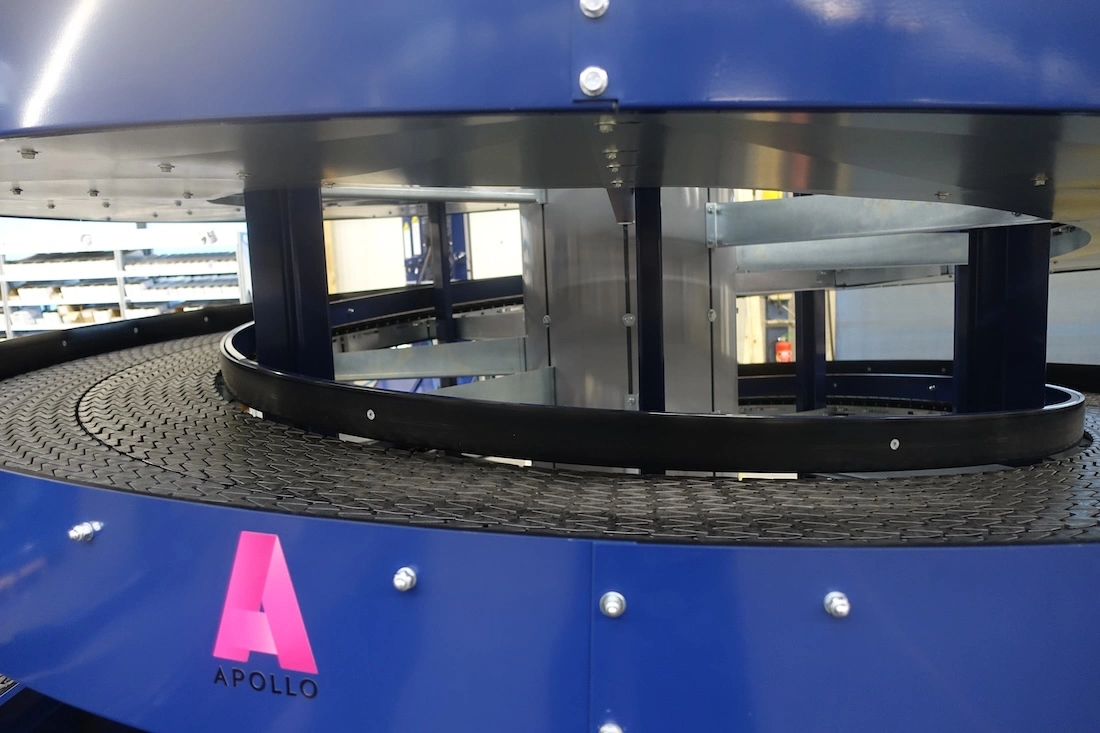
Since the Mass Flow runs on a single motor, energy consumption is low. This also aids in low maintenance, durability and a long life expectancy. Similar to our other Vertical Spiral Conveyors, the Mass Flow Spiral Conveyor is equipped with a guiding rail system for our conveying surface, including precision low friction bearings. The slats do not need supports or wear strips, so there’s only rolling friction. No lubrication is needed, which results in a low noise level, clean transport and less maintenance. Our Mass Flow design features nesting slats that create a smooth conveying surface that allows product to reliably be transferred on and off the Spiral. The conveyor can handle up to a high capacity of 2,000 units per minute, depending on the unit size and slat width. It is also equipped with extended in and outfeed sections to facilitate smooth side transfer to and from external conveyors. The Mass Flow Vertical Conveying System is designed to operate 24 hours a day, 7 days a week and delivers a reliable high continuous throughput.
What types of products can it be used for?
The Mass Flow Conveyor is especially suited for the food and beverage industry, easily conveying products such as beer bottles, soda cans, yoghurt cups, water bottles, wine bottles or plastic juice cans. They are also commonly specified when bottles or cans travel from a bulk depalletizer to the filler, or sending filled cans to the pasteurizer.
Types and models
The Apollo Mass Flow Spiral Conveyors consists of 4 standard models which can be customized to your specifications. They can also be modified in the field to accommodate emerging needs and requirements. All Spirals are equipped with an infeed and outfeed, which can be placed in different angles and can be extended to make the Mass Flow Spiral fit easily into most layouts. They are available in several slat widths and spiral diameters. Additionally, a the coating type can be selected – coated in a RAL colour of your choice or stainless steel). They can also be specified for operations in a wet environment.
In addition to the Mass Flow Spiral Conveyor System, we offer many more options for vertical conveying, such as the Single Lane Spiral Conveyor and the Narrow Trak Spiral Conveyor. If you would like to know which model Spiral Conveyor best suits your needs, feel free to contact us. We are always willing to work with you, so we can provide you with the best possible solution for your business.