Bucket Elevators

Bucket Elevators van Apollo
100mm | 200mm | 600mm
Standard | stainless steel | food grade | metal-detectable | anti-static
Bucket elevator features
Our Bucket Elevators can be configured with multiple inlets or outlets that feature selective bucket-tipping capabilities. This is accomplished by an air-actuated tipping ramp. The last tipping ramp is always in a fixed position, ensuring that all buckets are emptied.
Suitable for:

Product links:
Service
Though the products are designed to deliver high performance during a life time, no machine can operate without maintenance.
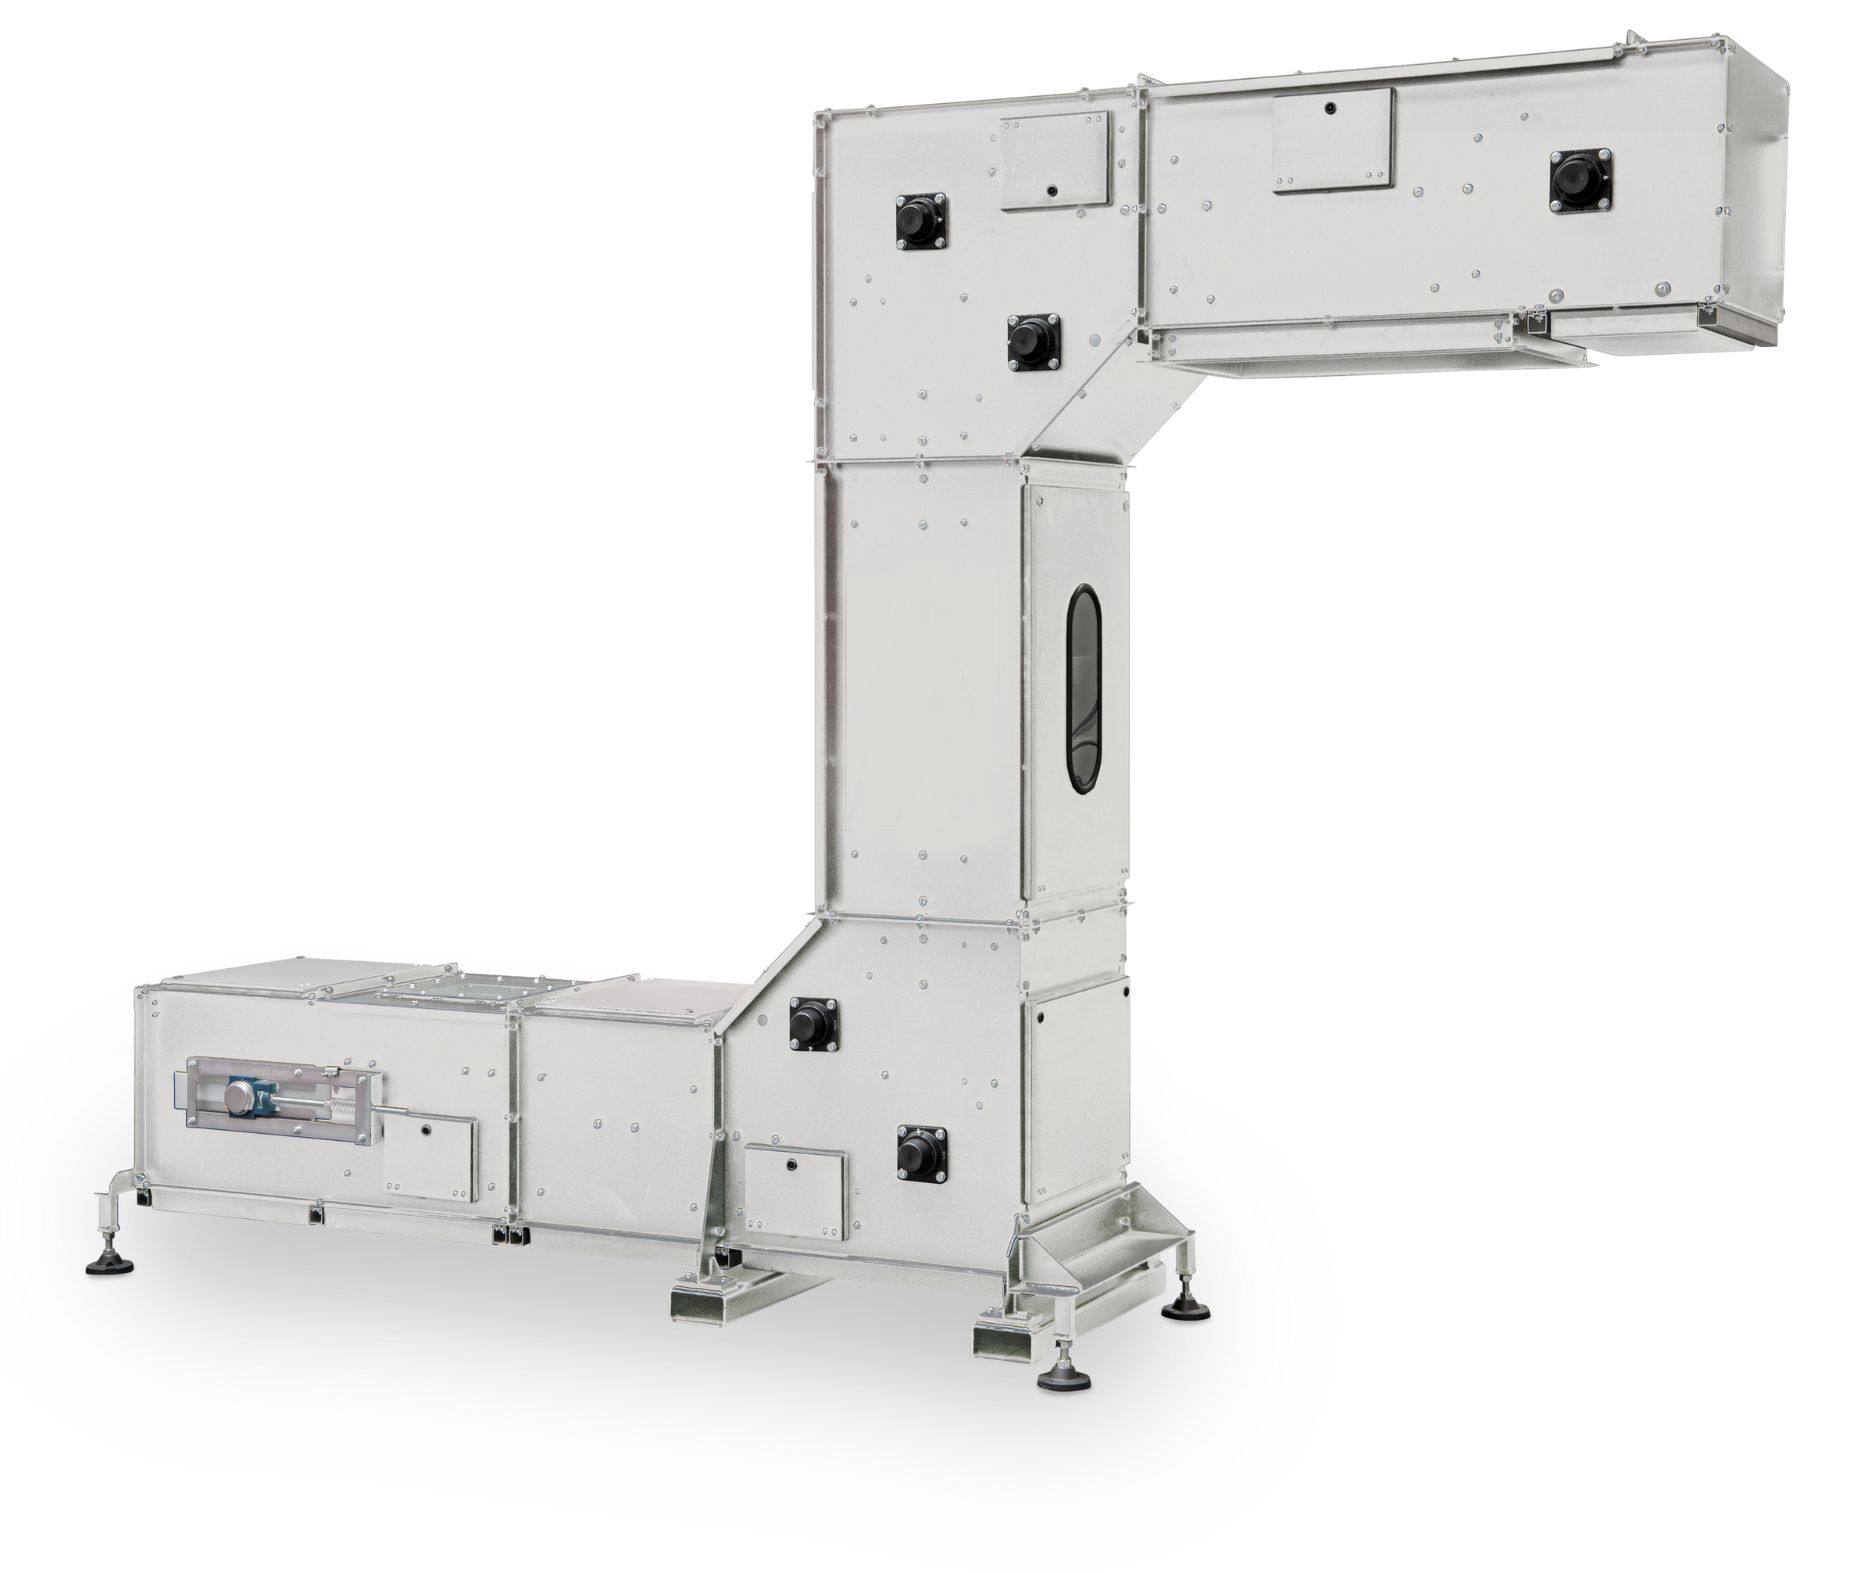
Combine vertical and horizontal transportation of bulk materials in one integral unit.
Apollo Bucket Elevators have earned a reputation for being the most durable bulk material conveyors in the marketplace. Their robust and forward-thinking design combines a number of features—from gentle handling and rugged construction to minimal maintenance and modular design—businesses have come to benefit from and deeply value.
Apollo Bucket Elevators’ main feature is that they are completely enclosed and have overlapping pivoting buckets, that help prevent spillage and keeps out foreign debris. Additionally, our Bucket Elevators stand out from our competitors because they are completely modular, have pivoting buckets and can have multiple inlets and outlets.
Our Bucket Elevators are designed for heavy-duty operations and have long lifespans. They can be delivered in powder-coated carbon-steel, stainless-steel or wet environment versions. Our Bucket Elevators can be configured with multiple outlets that feature selective bucket-tipping capabilities. This is accomplished by an air-actuated tipping ramp – The last tipping ramp is always in a fixed position, ensuring that all buckets are emptied.
Our Bucket Elevators are designed for gentle handling and ideally-suited to transport a broad range of bulk products in the food, agriculture, pharmaceutical, cosmetic, chemical, ceramic, glass, recycling, building, metallurgical and other industries.
Gentle Handling
Apollo Bucket Elevators are at robust completely enclosed design yet offer gentle handling of all kinds of products. These buckets overlap at the inlets to prevent spillage and can be selectively tipped at the outlets.
Rugged Construction
The chain is a 50mm plated roller chain with a hollow pin shaft and 28.5 mm diameter rollers. The rolling surface is made of polyurethane, providing smooth and quiet operation. The buckets are made of food-grade-reinforced polyamide, complying with U.S. Food and Drug Administration (FDA) standards and the European Food Safety Authority (EFSA). The buckets are molded in one piece and can handle temperatures from –20 to +93 degrees Celsius.
Additionally, flanges are provided at the inlets and outlets to facilitate easy attachment of extended funnels, shoots or tubes.
Low Maintenance
Apollo Bucket Elevators are built using high-quality components. As such, you can expect only minimal maintenance and down time. All our Bucket Elevator models have easily removable inspection covers and a conveniently located inspection window.
Our Bucket Elevators feature drawers located underneath the horizontal sections to facilitate fast and easy cleaning. The inside walls are smooth, helping prevent dust buildup. All bearings are mounted outside for easy access. Our Bucket Elevators are also equipped with a quick-release mechanism to facilitate fast installation or removal of buckets as well as an automatic chain tensioning device and built-in overload protection. A variable frequency drive, also known as a VFD, is required for proper operation.
Completely Enclosed
Our Bucket Elevators are completely enclosed, helping to mitigate foreign debris. Their construction also offers inspection windows and access ports to simplify cleaning and maintenance procedures.
Specs & Configuration

Most Common Models

Configurations
Apollo Bucket Elevators’ modular design enables us to customize with ease and makes your bucket elevator versatile as well as easy to install and modify. The most common configurations are our C and Z configurations, which are available with three different bucket sizes, yielding capacities up to 10, 23 or 59 cubic meters per hour. The buckets must be loaded with a controlled volume and across the full width of the buckets.
No matter the use case, our team is up to the challenge of finding solutions your business needs. Explore a special application for a custom-built bucket elevator we created for a customer needing to elevate lightweight cellulose material. You can also Download a printable RFQ Form.
Gentle handling - horizontal-vertical
The pendulum bucket elevator is used for very gentle vertical conveying of all kinds of granular products. This conveyor has the benefit of combining both horizontal and vertical transport in one machine. Adding the very gentle way of transporting, the pendulum bucket elevator is the perfect conveyor for seeds and other sensitive products. By means of using different speeds, there’s a wide range of different hourly capacities that can be reached which goes up to 60 m3/h.
Dust control bucket elevators
The bucket elevator is designed for extremely high dust levels even when the product is highly abrasive. Through optimally positioned suction points, dust-tight bearings and anti-static buckets pollution levels remain very low which contributes to machine reliability and low maintenance. Bucket elevators are mainly used in the agriculture-, food-, and industry sector.
Features and benefits
Chain tensioning via manual spindles ensures high machine durability.
The incoming product is fed to the pendulum Bucket Elevator continuously or batch wise. The edges of the buckets overlap each other in the inlet section and therefore prevent spillage of kernels.
A sensor detects the rotation of the sprocket. In case of a chain breakage, the Bucket Elevator will be switched off to avoid further damage.
- Long life, high-tensile, chromated chain, with steel or nylon rollers (noise reduction)
- Chain also available in stainless steel with stainless steel rollers
- Standard buckets glass fibre reinforced polyamide
- Buckets in compliance with food grade standards, FDA and EC 1935/04
- Anti-static or detectable buckets are optional
The number of outlets is flexible. The last outlet is always fixed to tilt and unload, while additional ones can be pneumatically actuated separately. These additional outlets further optimise conveying flexibility and enhance product handling.
Solely high quality components are used to ensure optimal durability and minimal down-time. Geared motors on our Bucket Elevators are supplied by SEW. Their renown low power requirements reduce energy consumption and eventually costs.
An overload switch fitted on the drive station stops the drive immediately if abnormal torque is experienced, preventing possible machine damage.


Industries
Bucket Elevator Agriculture
Bucket Elevator Food
Bucket Elevator: Industry
Get in touch with us
Apollo Group will reply as quickly as possible, “*” indicates required fields
"*" indicates required fields
Frequently asked questions:
What is a bucket elevator?
A bucket elevator is a vertical transport system used to move bulk goods such as grains, minerals, powders or fertilisers from a lower to a higher point. The system consists of a belt or chain to which buckets are attached at regular intervals.
Bucket Elevator or Spiral conveyor: which one do I need?
A spiral conveyor moves unit loads such as cases, crates, totes and bags vertically on a continuous helical track. A bucket elevator lifts loose bulk material such as grains, pellets or coffee beans in enclosed buckets. We build both, so the choice depends on whether your product arrives packaged or as free-flowing bulk.
What are the advantages of bucket elevators?
Bucket elevators offer interesting advantages because they can efficiently and continuously transport bulk materials vertically with a compact design that takes up little floor space, which is ideal for space constraints in factories. They ensure a controlled material flow, reduce dust formation and material loss thanks to their closed construction, which increases safety and cleanliness.
How does a bucket elevator work?
Bucket elevators work very simply: there are buckets attached to a belt or chain, which move up and down between the top and bottom. At the bottom, the buckets pick up the material, for example grain kernels, and then lift it up. At the top, the buckets tip the material out so that it can be transported further. Because the material remains in the buckets, little dust is released and almost nothing is lost. This allows them to quickly transport large quantities of material upwards without creating a mess.
Can a bucket elevator transport material both horizontally and vertically?
Yes. Our bucket elevators combine horizontal and vertical transport in one enclosed machine. In the C and Z configurations, the pivoting buckets stay level as they travel from the horizontal inlet section, up the vertical section and along the horizontal outlet section. One machine replaces a separate conveyor and elevator, with fewer transfer points and less spillage.
Which materials can a bucket elevator handle?
Our bucket elevators handle free-flowing granular bulk products: grains, seeds, nuts, coffee, confectionery, pet food, recycled plastics, wood pellets and small metal parts. The one-piece polyamide buckets work at product temperatures from -20 to +93 °C. Wet, sticky or paste-like products that do not release cleanly from a bucket need a separate assessment, which we do per application.
What is the difference between centrifugal discharge and pivoting buckets?
In a centrifugal bucket elevator, the buckets throw the material out at the head pulley, which can break fragile products. Our elevators use pivoting buckets that stay level during transport and are tipped by a ramp at the outlet. Extra outlets have air-actuated ramps, so you choose where the product is discharged. The last ramp is fixed, so every bucket is always emptied.
Belt or chain bucket elevator: which is better?
Belt elevators are common in high-capacity grain handling, where the buckets run on a rubber belt. A chain is stronger and allows pivoting buckets that combine horizontal and vertical transport in one machine. Our bucket elevators run on a 50 mm plated roller chain with a hollow pin shaft, also available in stainless steel with stainless steel rollers.
What capacity can a bucket elevator reach?
Our C and Z configurations come with three bucket sizes and reach capacities of up to 10, 23 or 59 m³ per hour. The pendulum bucket elevator reaches up to 60 m³ per hour, depending on the chain speed. The actual capacity depends on the bulk density and particle size of your product and on how evenly the buckets are filled.
How do I choose the right bucket elevator for my application?
Start with four figures: the required capacity in m³ per hour, the bulk density and particle size of your product, the lift height and the number of inlets and outlets. The buckets must be filled with a controlled volume across their full width, so the feeding method matters as well. Send these details through our RFQ form and we propose a configuration.
Are your bucket elevators suitable for food applications?
Yes. The standard buckets are made of glass fibre reinforced polyamide and comply with FDA regulations and EU Regulation (EC) 1935/2004 for food contact materials. For stricter hygiene requirements we supply stainless steel versions, stainless steel chains and metal-detectable buckets. Smooth inner walls, inspection windows and cleaning drawers keep the machine easy to clean.
How much maintenance does a bucket elevator need?
Our bucket elevators need little maintenance thanks to their enclosed design and high-quality components. Removable inspection covers and an inspection window give quick access. Cleaning drawers under the horizontal sections, externally mounted bearings and quick-release buckets save time during service. Chain break detection and an overload switch stop the drive before damage occurs. Our service department handles inspections and spare parts.
Can a bucket elevator handle dusty products safely?
Yes. Our dust control bucket elevator is built for high dust levels, including abrasive products. Optimally positioned suction points, dust-tight bearings and anti-static buckets keep dust emissions low and the machine reliable. The fully enclosed housing keeps dust in and foreign debris out. For installations in ATEX zones, we discuss the requirements for your situation before we quote.